CNC Turning
If it is round, we can turn it.
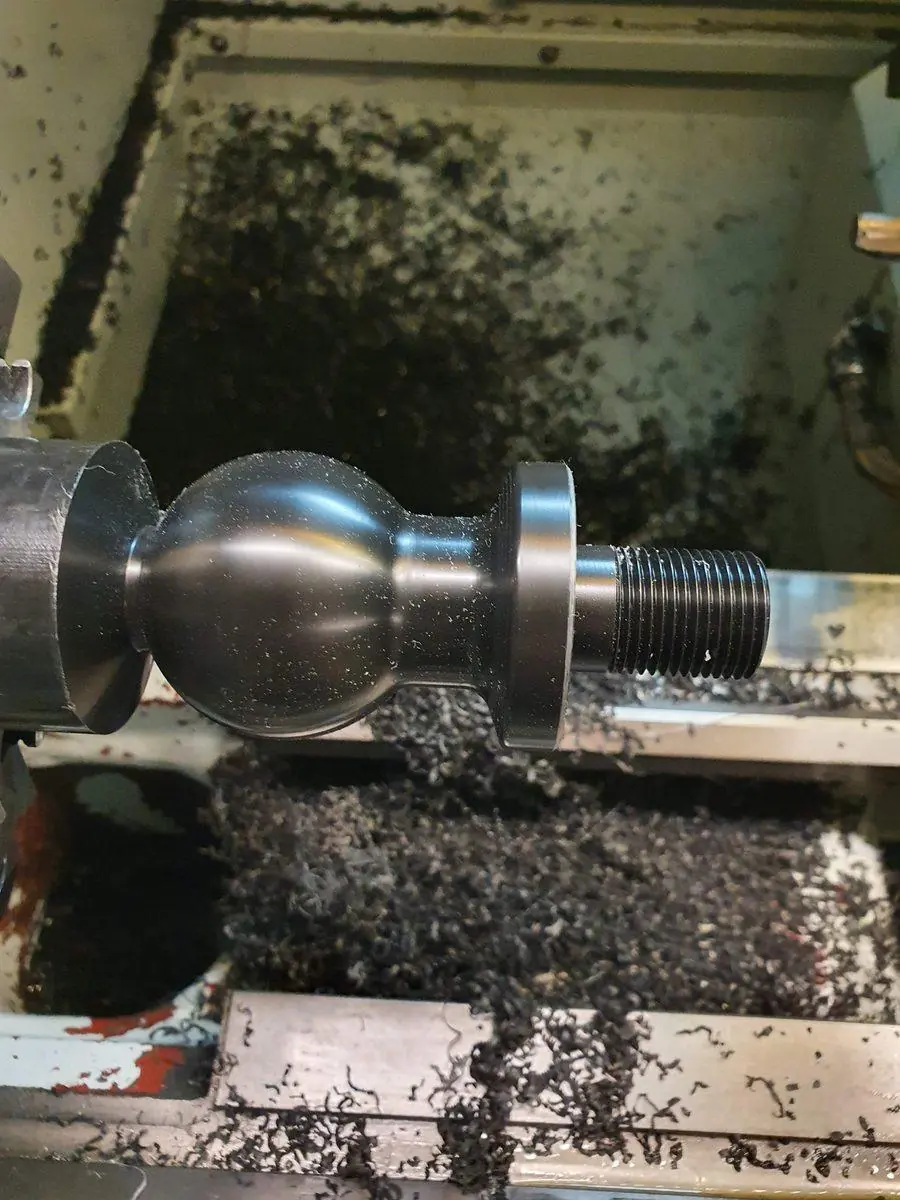
CNC turning is where a lot of our work lives. The part spins in the chuck, the tool moves against it, and you end up with accurate diameters, clean bores and threads that fit properly the first time.
What we turn
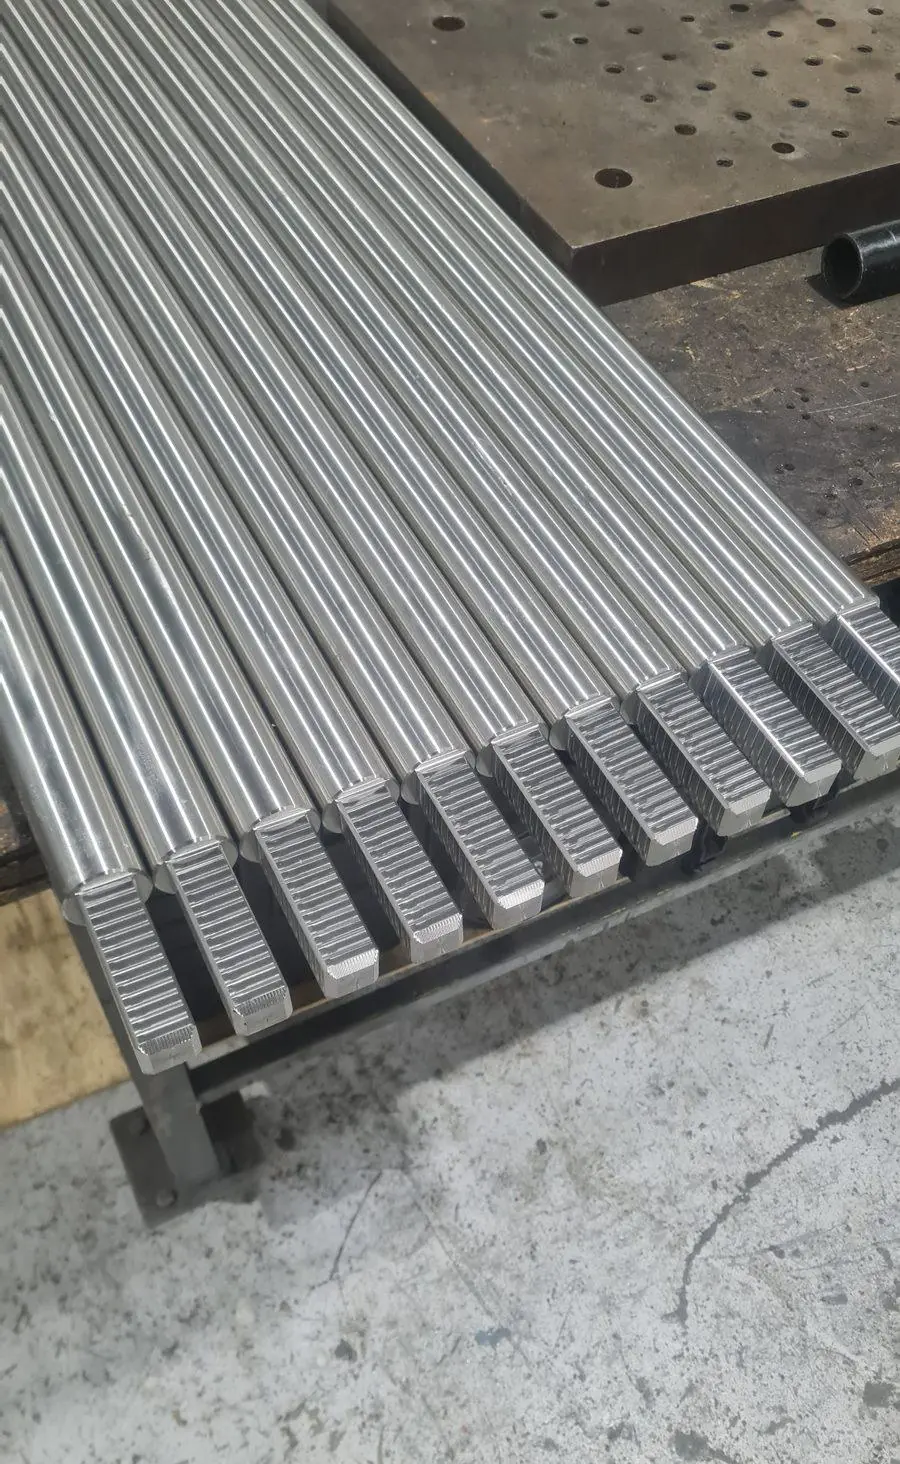
- Shafts — drive shafts, pump shafts, stub axles, spindles, pivot pins
- Bushes and sleeves — bronze, steel or stainless, to your bore and OD, including re-sleeving worn housings
- Spacers, collars and washers — the boring parts that hold everything else together
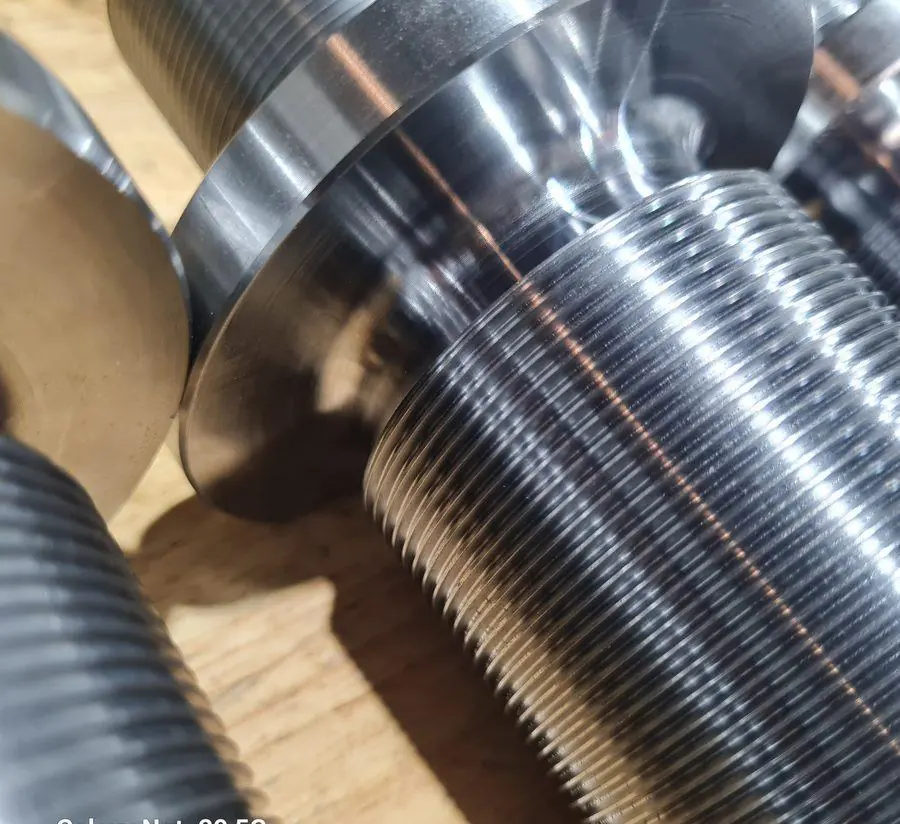
- Threaded components — studs, adaptors, glands, nipples, custom fasteners in metric and imperial
- Bored and reamed parts — bearing seats, housings and anything that has to take a press fit
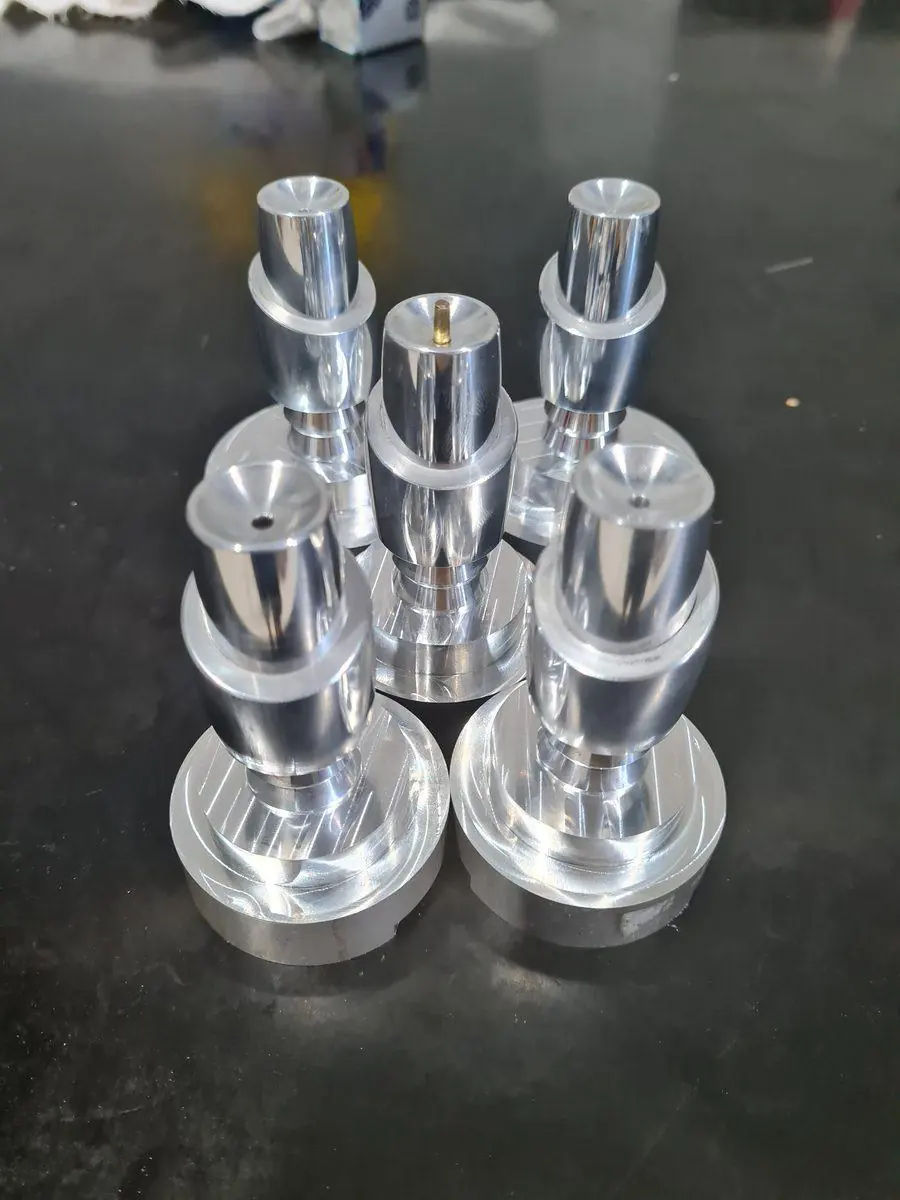
- Crimping die blanks and finished dies — hex and round, in ongoing batches
- Tapers, radii and profiles — anything the drawing calls for
Round parts for machines that have stopped
A large share of turning work here is replacement. A shaft has sheared, a bush has worn oval, a spindle has picked up. The machine is down and nobody can find the part any more.
Bring the old one in. We measure it, work out where it failed, and make a new one — usually in a better material than the original. Worn bores get re-sleeved: we bore out the damaged housing, turn a sleeve to suit, press it in and machine it back to size. Cheaper than a new housing and often stronger than the original.
Materials
4140 heat-treated for shafts and pins that take real load. 316 stainless for anything near salt water — boat fittings, marine hardware, washdown equipment. Tool steels for dies and wear parts. Aluminium where weight matters or the part is a prototype.
If you are not sure what the part should be made of, tell us what it does, what it bolts to and where it lives. That is enough for us to recommend something sensible.
Threads
Metric coarse and fine, imperial, UNC and UNF, BSP and NPT pipe threads, and single-point threading for anything odd or non-standard. If you have got an old part with a thread nobody stocks, we can copy it.
Left-hand, multi-start, ACME and trapezoidal, and mining threads — rope threads and drill-rod threads — are all things we have cut. Todd spent three years at Sandvik's mining tooling plant, so an odd thread form does not slow us down.
Capacity
CNC lathe: 250mm swing, 300mm turning length in the chuck, 50mm bar through the spindle — so a shaft up to 50mm diameter and 3 metres long can be fed through the spindle and turned on a steady rest. Manual lathe: 400mm swing and 1.5 metres between centres for bigger diameters. We also straighten shafts and straighten stock before we turn it, which matters on anything long.
One-offs and batches, same shop
We will turn a single part for you. We will also turn the same part every month for the next five years — that is exactly what we do with crimping dies for electrical manufacturers, in repeat batches, run overnight.
Repeat turned parts are the ideal fit for our lights-out running. Once the job is programmed and the workholding sorted, the machine will cut them through the night, which brings the per-part price down and makes the delivery date dependable. See production machining.
Send a drawing or a photo of the round part you need, or drop the old one in at 12 George Road, Salamander Bay. Ring 0478 790 631. Get a quote →